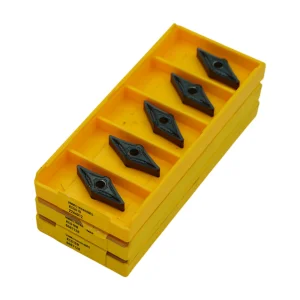
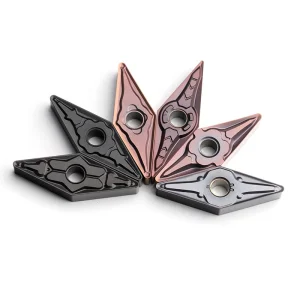
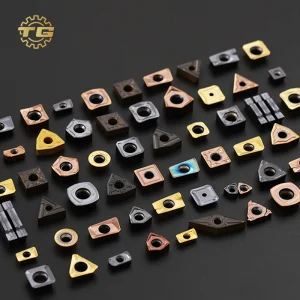
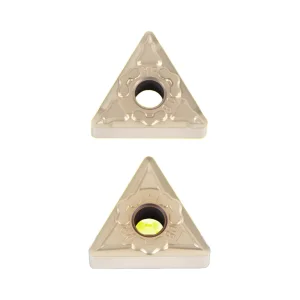
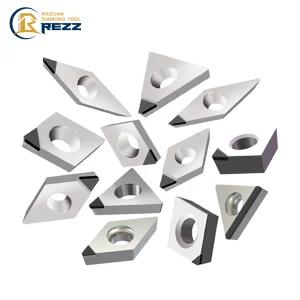
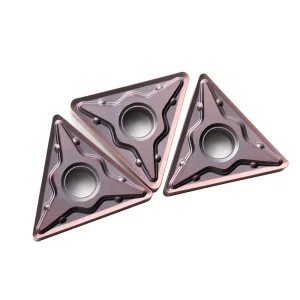
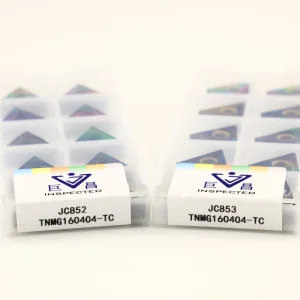
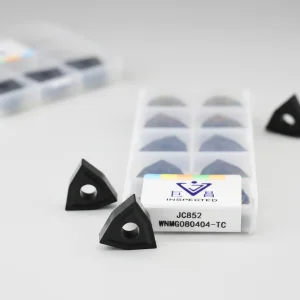
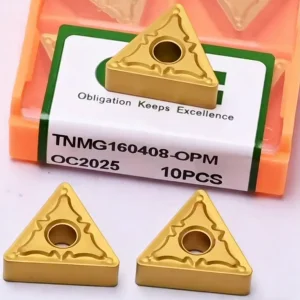
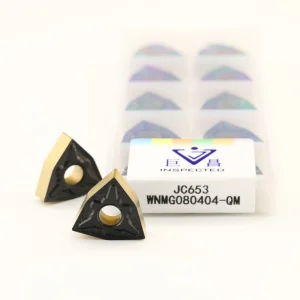
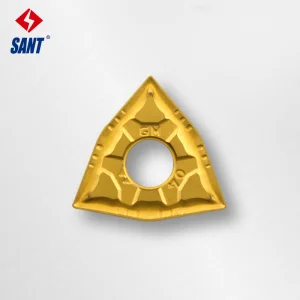
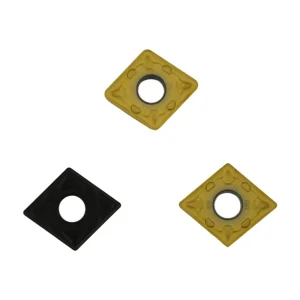
engineered for high-speed cutting, optimal chip control, and extended tool life across steel, stainless steel, and hardened alloy turning applications.
Analyzing Northern Albania’s economic growth, infrastructure investments, and the evolving tooling requirements of regional manufacturing hubs.
Shkodër, serving as the cultural and economic epicenter of Northern Albania, has experienced a decisive industrial structural transformation over recent years. Historically recognized for light manufacturing, textiles, and wood processing, the municipality of Shkodër and its surrounding industrial corridors (connecting toward Lezhë and the Montenegrin border) are rapidly emerging as a critical region for mechanical engineering, metal fabrication, automotive sub-assembly manufacturing, and public works infrastructure equipment maintenance.
The strategic proximity of Shkodër to major European transport routes via the Adriatic coast has drawn foreign direct investment (FDI) and encouraged domestic entrepreneurs to establish sophisticated machine shops. Modern machine shops in Shkodër are increasingly equipped with 3-axis to 5-axis CNC lathes, Swiss-type automatic turning centers, and heavy-duty manual lathes focused on small-to-medium serial production and high-precision custom engineering.
Key Insight for Shkodër Procurement Managers: As local factories shift from repair work to original equipment component manufacturing (OEM) for Italian, German, and Central European supply chains, the tolerance requirements for turned parts have tightened to micro-levels ($\pm0.005 \text{ mm}$). Achieving such precision consistently requires ultra-stable indexable carbide inserts engineered with gradient substrates and thermal shock resistance.
How advanced PVD/CVD nanocoatings, substrate micro-structures, and chipbreaker geometries revolutionize metal removal rates (MRR).
Modern lathe turning inserts utilize multi-layer CVD (Chemical Vapor Deposition) coatings consisting of thick $\alpha\text{-Al}_2\text{O}_3$ and Medium Temperature TiCN for high-speed continuous steel turning, alongside ultra-thin, tough PVD (Physical Vapor Deposition) AlTiN/TiAlN coatings designed for interrupted cuts and stainless steel machining.
Engineered with ultra-fine tungsten carbide ($\text{WC}$) grain structures combined with tailored Cobalt ($\text{Co}$) binder ratios (6% to 10%), providing an exceptional balance between plastic deformation resistance at the cutting edge and high fracture toughness under shock loads.
Custom-designed chipbreaker geometries (e.g., -SF for ultra-finishing, -MS for medium stainless turning, -GH for heavy-duty roughing) effectively curl and break metallic swarf, eliminating bird-nesting long chips that damage workpiece surfaces and endanger CNC operators.
| ISO Group | Material Category | Recommended Grade | Coating Architecture | Cutting Speed ($V_c$) | Primary Application in Shkodër |
|---|---|---|---|---|---|
| P (Steel) | Carbon Steel, Alloy Steels (e.g., 4140, 1045) | DF-P25 / IC907 | CVD TiCN + $\text{Al}_2\text{O}_3$ + TiN | 180 – 320 m/min | Drive shafts, hydraulic cylinder pins, gear blanks |
| M (Stainless) | Austenitic & Duplex (304, 316L, 2205) | DF-M20 / TiAlN | PVD Nano-AlTiN | 140 – 240 m/min | Hydro-turbine fittings, food processing components |
| K (Cast Iron) | Grey Iron, Ductile Iron (GG25, GGG40) | DF-K15 / CVD | Thick $\text{Al}_2\text{O}_3$ Ceramic Coating | 200 – 380 m/min | Brake drums, pump housings, flywheel castings |
| H (Hardened) | Hardened Tool Steel (HRC 45-65) | DF-H10 / PCBN | PVD TiAlN / CBN Tipped | 80 – 160 m/min | Stamping dies, reconditioned wear plates, bearings |
Bridging Chinese high-tech manufacturing capacity with European engineering standards for Shkodër exporters.
In today's volatile global supply chain landscape, machine shops and procurement leaders in Shkodër cannot afford unexpected tooling delivery delays or unpredicted batch-to-batch quality deviations. Zhejiang DentFix Tool Co., Ltd. leverages China’s apex industrial infrastructure, combining raw material security with fully automated Industry 4.0 smart factory production lines.
All DentFix carbide inserts undergo High-Pressure Hot Isostatic Pressing (HIP) at 1500°C and 100 bar pressure. This eliminates internal micro-porosity, guaranteeing 100% theoretical density and preventing catastrophic edge breakage under heavy mechanical stress.
Our automatic peripheral grinding centers maintain dimensional tolerances down to $\pm0.002 \text{ mm}$. Edge hone radii are applied with robotic precision to ensure optimal chip flow and razor-sharp edge integrity.
We provide full-spectrum OEM labeling, custom chipbreaker design, and expedited direct freight solutions to Albania, enabling Shkodër distributors to lower Total Cost of Ownership (TCO) by up to 40%.
Examine how our indexable turning inserts optimize metal cutting operations across local industrial environments.
Location: Industrial Zone, Shkodër
Workpiece: AISI 316L Stainless Steel Hydromechanical Shafts
Challenge: Excessive built-up edge (BUE) and rapid flank wear using traditional inserts during continuous turning.
Solution: Implemented DentFix CNMG120408-TF IC907 with PVD Nano-TiAlN coating. Resulted in 180% longer tool life and smooth chip evacuation without surface tearing.
Location: Metal Stamping Facility, Shkodër Region
Workpiece: SKD11 Cold Work Tool Steel Guide Rings
Challenge: High tool wear rate and thermal cracking during dry rough turning.
Solution: Deployed Premium Tungsten Carbide Inserts HRC45-55 Coated Series with ultra-fine substrate. Machining stability increased, eliminating secondary grinding operations.
Location: Machinery Maintenance Workshop, Shkodër
Workpiece: Ductile Iron (GGG40) Flanged Housing Castings
Challenge: Insert corner chipping due to severe intermittent impact cuts on raw cast surfaces.
Solution: Utilized WNMG080408-QM CVD Coated Grade. Achieved consistent edge toughness, boosting parts per cutting edge from 35 to 90 pieces.
A premier global manufacturer committed to quality, precision, and state-of-the-art CNC tooling technology.
Zhejiang DentFix Tool Co., Ltd. is a professional manufacturer specializing in the research, development, production, and global distribution of precision CNC cutting tools and carbide solutions. Since its establishment, the company has been committed to providing high-performance tooling products for the metalworking industry, serving customers across automotive, aerospace, mold & die, general engineering, energy, and precision manufacturing sectors.
Driven by continuous innovation and customer-focused development, DentFix has grown into a modern manufacturing enterprise that integrates R&D, intelligent production, quality control, sales, and technical support. The company has built a strong reputation for delivering reliable products, consistent quality, and professional services to customers in both domestic and international markets, including growing partnerships across Shkodër and the broader Balkan peninsula.
With advanced manufacturing technologies, experienced engineering teams, and strict quality management systems, DentFix continuously improves its product performance and production efficiency. Guided by the principles of Quality First, Innovation, Reliability, and Customer Satisfaction, we empower our clients to achieve maximum productivity and minimized tooling expenses.
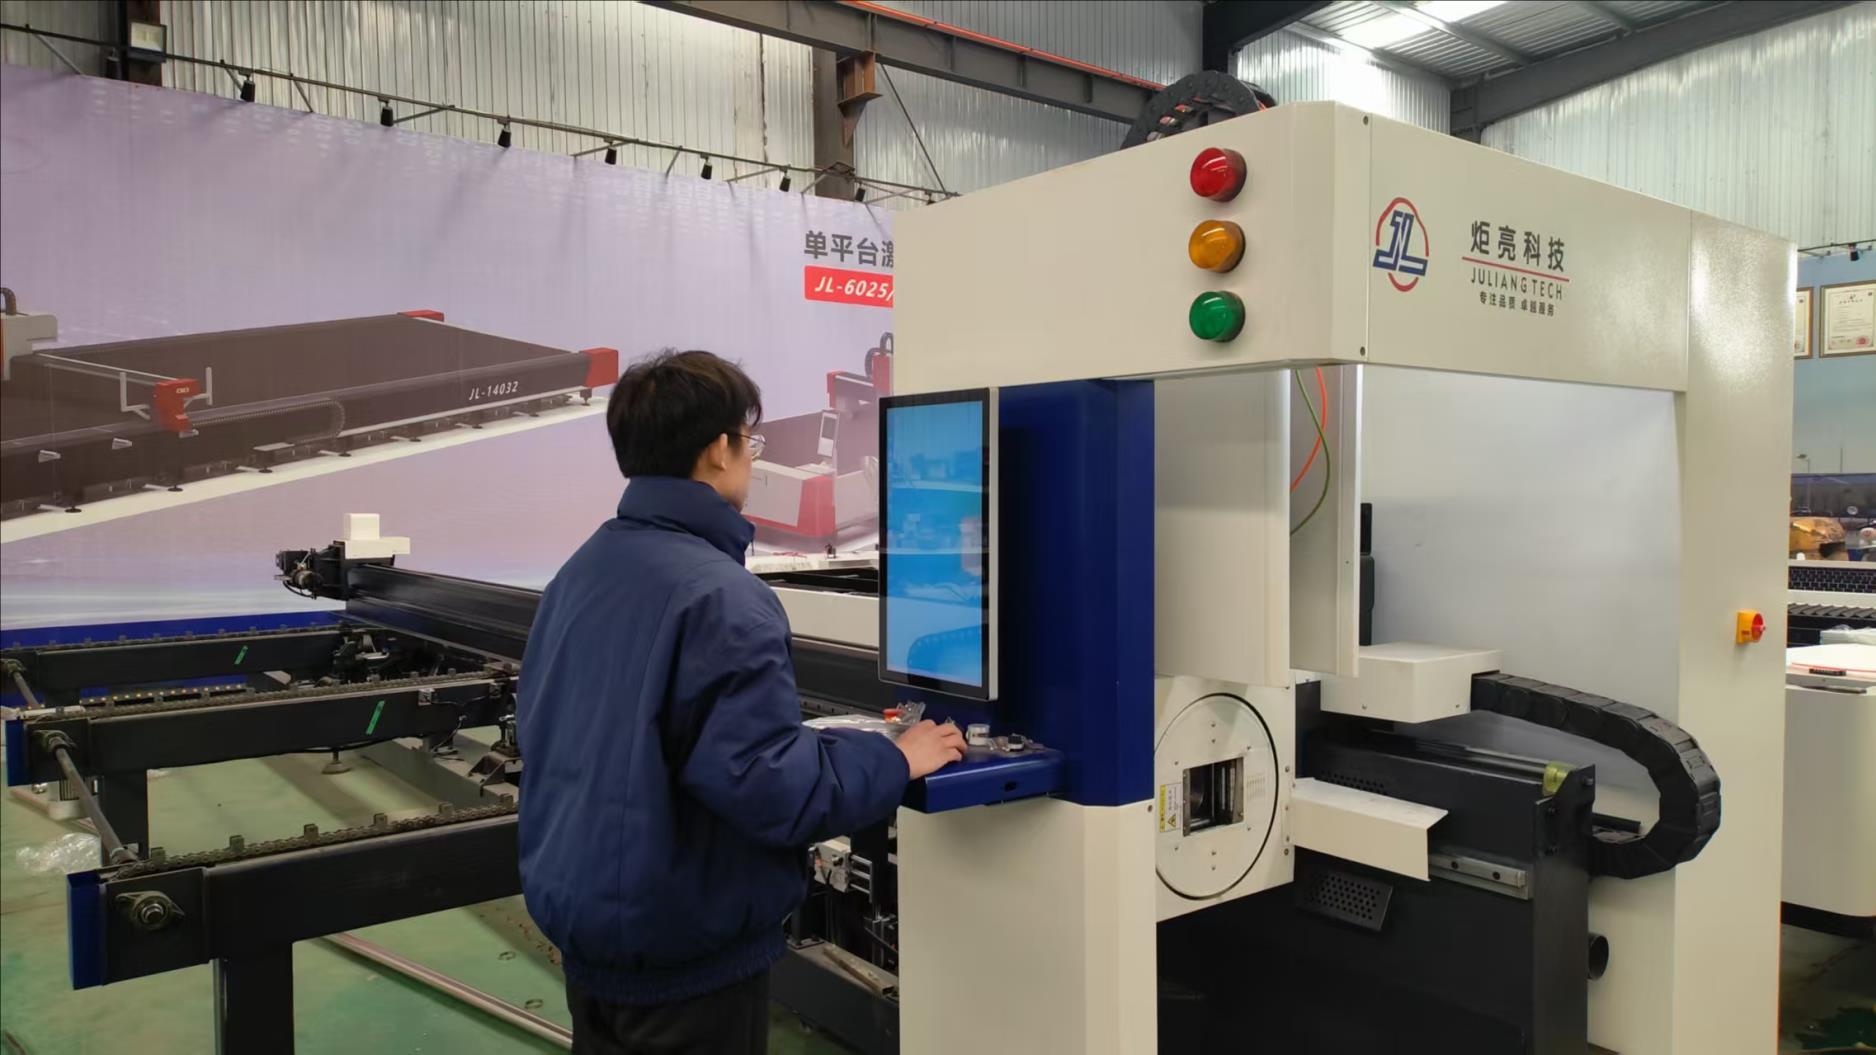
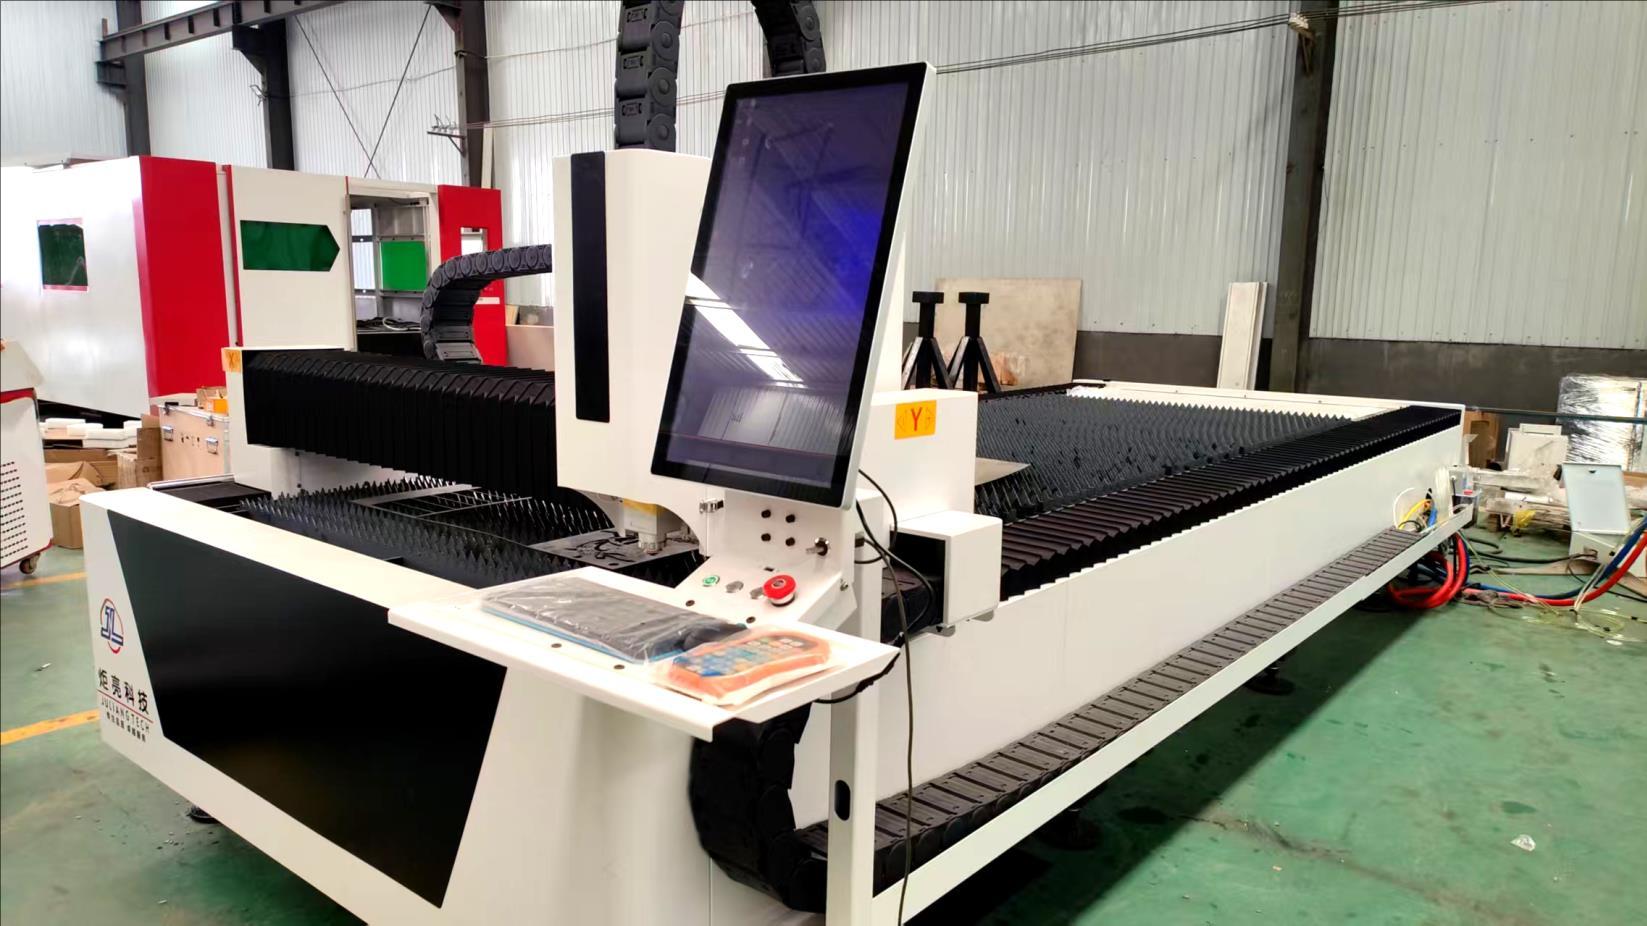
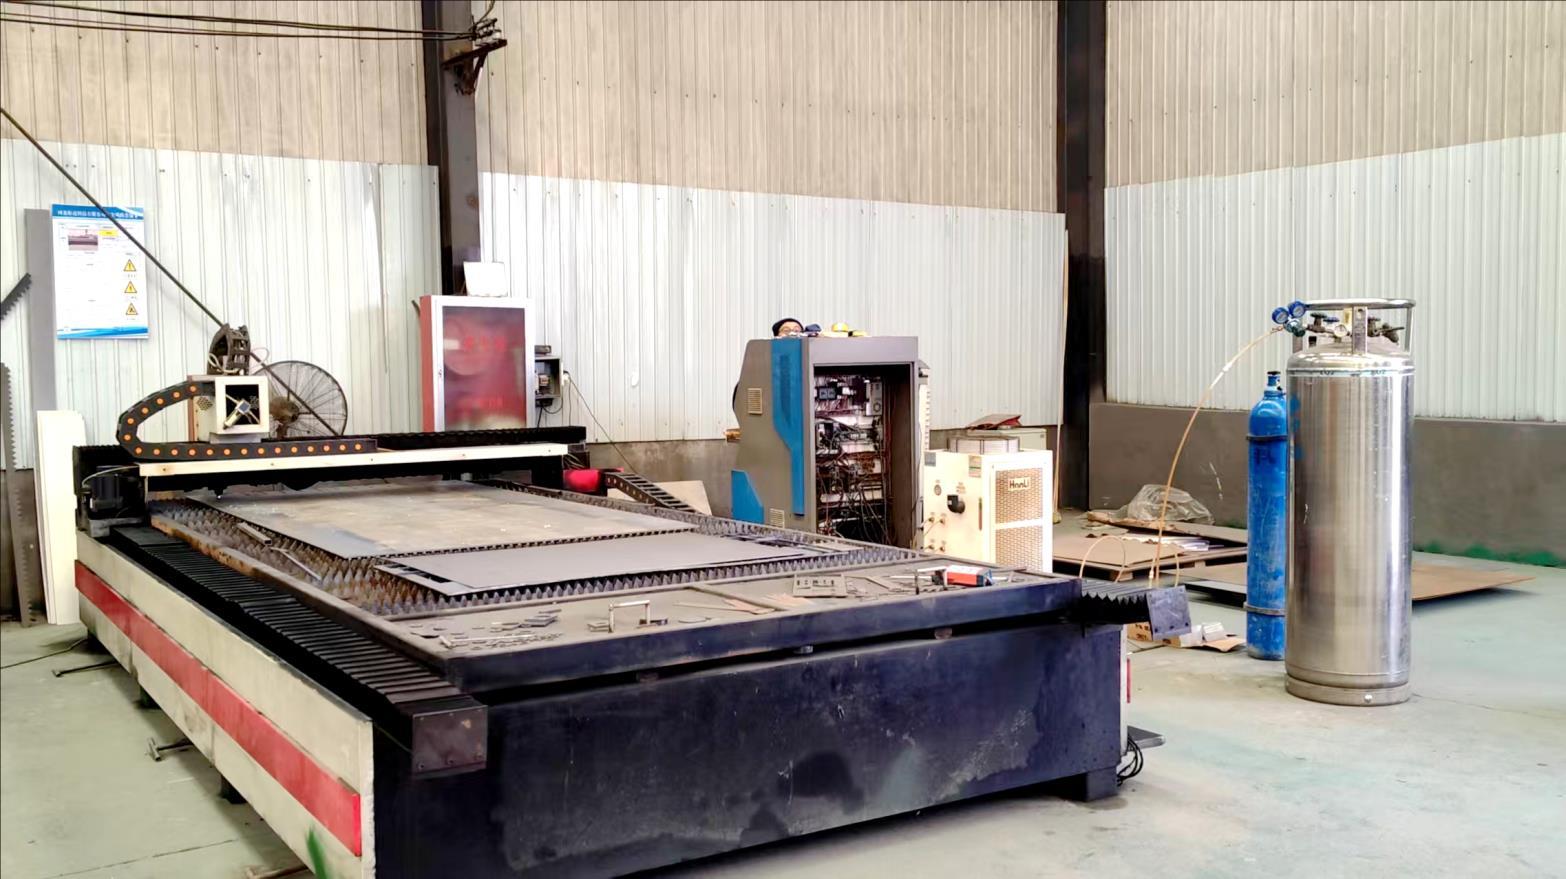
Explore our full line of indexable turning inserts, thread cutters, and milling solutions available for immediate export to Shkodër.
Expert answers on tooling selection, chipbreaker matching, and optimizing cutting parameters for machine shops serving Shkodër.
Select CVD coatings (thick $\text{TiCN} + \text{Al}_2\text{O}_3$) for medium-to-heavy roughing operations and high-speed continuous dry/wet turning of carbon steels where high thermal insulation and crater wear resistance are needed. Choose PVD coatings (nano-TiAlN/AlTiN) for interrupted cutting, stainless steel, sticky materials, or fine precision finishing where sharp cutting edges and high edge toughness are paramount to prevent micro-chipping.
Standard ISO turning inserts (CNMG, WNMG, DNMG, TNMG) in default grades are kept in extensive stock for immediate air dispatch, arriving in Albania within 5–9 business days via express courier (DHL/FedEx). Dedicated container or wholesale shipments to Durrës or Shkodër logistics hubs take approximately 22–28 days.
Austenitic stainless steels (e.g., 304, 316) tend to work-harden rapidly and produce continuous stringy swarf. Utilizing specialized positive chipbreakers (such as -MS or -MM) creates optimal shearing angles that lower cutting forces and break swarf into tight C-shaped chips, preventing workpiece scratch defects and reducing heat accumulation on the cutting edge.
Yes. Zhejiang DentFix Tool Co., Ltd. features comprehensive in-house tooling design and 5-axis CNC grinding capability. We accept OEM/ODM orders based on customer CAD drawings, providing custom corner radii, special nose geometries, and custom coating layer formulations tailored for unique machining challenges.
Flank wear appears as a smooth, uniform abraded land along the cutting edge caused by mechanical friction; it can be mitigated by reducing cutting speed ($V_c$). Thermal cracking presents as vertical comb-like cracks perpendicular to the edge caused by rapid temperature cycling during intermittent wet machining; it is fixed by applying high-toughness PVD grades or switching to dry machining with compressed air cooling.
Maintain strict center-height alignment of the toolholder, select an appropriate anvil/shim angle matching the thread lead helix angle, and apply an infeed method such as modified flank infeed (1° to 3° angle) to ensure single-edge cutting and clean chip clearance during deep thread passes.
Partner with Zhejiang DentFix Tool Co., Ltd. for factory-direct precision indexable turning inserts, competitive wholesale pricing, and dedicated engineering support.
Send Inquiry Now DentFix Tool