7 Best Ways to Fix Chatter Marks in Metal Milling?

Time:2026-09-06 Author:Charlotte
0%

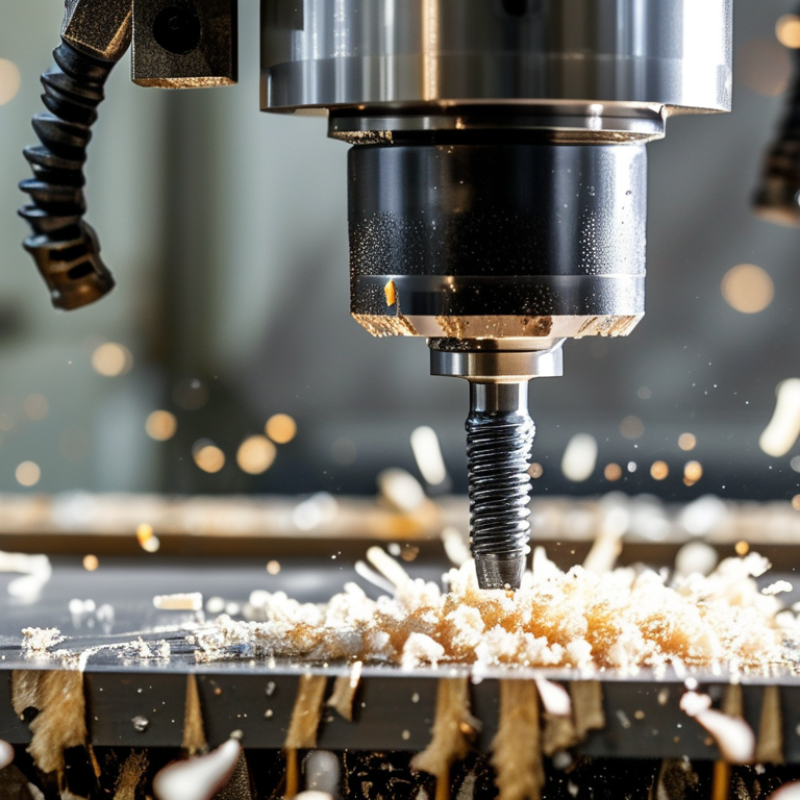
Chatter marks can turn a clean aluminum wall into a washboard of ridges within seconds. The high-pitched squeal is more than an unpleasant sound. It often signals unstable cutting, excessive tool deflection, or a weak machine-tool setup. Learning how to fix chatter marks in metal milling requires more than lowering the spindle speed and hoping for improvement.

Tony Schmitz, a respected researcher in machining dynamics, explains the issue clearly: “Chatter is a dynamic problem, not merely a cutting-parameter problem.” His statement matters because the same end mill can cut quietly in one setup and vibrate badly in another. Tool stick-out, holder runout, workholding pressure, material hardness, and radial engagement all influence the result.

This guide examines seven practical ways to reduce or remove chatter marks. It covers checking tool and holder condition, shortening overhang, improving workholding, adjusting spindle speed, changing feed per tooth, reducing radial or axial engagement, and using stability-lobe data when available. A small speed change may help. Sometimes it makes the surface worse.

Do not trust sound alone. Inspect the tool edge, measure runout, and compare the finished wall under consistent lighting. A cutting chart offers a starting point, not a guarantee. Real machines have worn bearings, imperfect fixtures, and different structural behavior. That is where many recommendations become unreliable.

The goal is not simply a quieter cut. It is a stable process that leaves predictable surfaces, protects the cutter, and produces measurable improvement. Expect some trial and error. Record each change carefully.
7 Best Ways to Fix Chatter Marks in Metal Milling?

Identify the Main Causes of Chatter Marks in Metal Milling

Chatter marks usually begin with vibration, not a poor finishing pass. The main causes are low system rigidity, excessive tool overhang, unstable spindle speed, and aggressive cutting depth. A 2022 review in the International Journal of Machine Tools and Manufacture identifies regenerative vibration as a key mechanism. Each tooth repeats a previous wave on the workpiece. That changing surface then alters the next cut.

Check the whole cutting system. A slender end mill, loose workholding, or a thin wall can amplify vibration. Tool runout matters too. Even small runout makes one tooth cut harder than the others. Research reported in CIRP Journal of Manufacturing Science and Technology links tool dynamics and runout with uneven chip thickness and roughness growth. The U.S. Department of Energy’s Industrial Assessment Center guidance also emphasizes reducing unnecessary cutting force and improving fixture stiffness.

Look at the marks closely. Regular waves often indicate a speed near the system’s natural frequency. Random tearing may suggest a worn edge, built-up material, or poor chip evacuation. Reduce tool overhang before changing everything else. Then test a lower radial engagement or a different spindle speed. Keep feed per tooth consistent during each trial. Do not trust a calculator blindly. Real assemblies rarely match catalog stiffness. I have seen operators blame coolant first, although the fixture was flexing visibly. That mistake costs time. A simple dial-indicator check, short overhang, and measured tool runout can reveal more than another finishing pass.

Stabilize the Workpiece, Tool, and Machine Setup

Chatter marks often begin with movement that feels too small to notice. Stabilize the workpiece with firm, even clamping, and support thin walls with a suitable fixture or temporary backing. Keep the tool overhang as short as practical. Long stickout acts like a spring.

Tool stability matters just as much. Check holder seating, tool runout, and insert security before changing cutting data. A sharp, balanced tool usually leaves a cleaner surface. Reduce unnecessary tool length. Also inspect the spindle taper and fixture contact surfaces. Small chips trapped under a fixture can create visible waves.

Machine behavior completes the setup. Lock unused axes, verify table and vise rigidity, and avoid cutting near the edge of the machine’s working range. If marks remain, adjust spindle speed in small steps, then review feed per tooth and radial engagement. I have sometimes blamed the cutter too quickly. The real problem was a flexible workpiece. That mistake is worth remembering. Listen for a steady cutting sound, watch the toolpath, and measure the finished wall instead of trusting appearance alone. Chatter may disappear on one side and remain on another. That difference usually reveals uneven support or changing engagement.

Optimize Cutting Speeds, Feeds, and Depths

Chatter marks usually indicate unstable cutting, not merely a dull tool. Start by lowering spindle speed in small steps, often 10 to 20 percent. Test each change on scrap material. A stable cutting zone may appear suddenly. If reducing speed fails, raise it carefully instead. Some setups chatter at one frequency and cut smoothly at another. This reversal is easy to miss.

Match feed rate to chip load, tool diameter, and tooth count. A light feed can rub, heat the edge, and increase vibration. A heavy feed can overload the cutter and deflect the workpiece. Adjust feed per tooth instead of guessing from machine feed alone. Reduce radial engagement when the cutter is heavily buried. Keep axial depth moderate, especially with long tools or thin walls. Shorter tool stickout often produces the fastest improvement.

Use a rigid holder, verify clamping, and clear chips from the cutting area. Change the toolpath direction when entry or exit creates sudden engagement. For finishing, leave a small and consistent allowance. Changing every setting together is a common mistake. You will not know which correction worked. Record speed, feed, radial engagement, axial depth, and cutting sound during each test. A quieter cut with slightly lower material removal may be the more reliable choice. Tool geometry and workholding can still defeat perfect numbers.

7 Best Ways to Fix Chatter Marks in Metal Milling? - Optimize Cutting Speeds, Feeds, and Depths

Method Typical Chatter Cause Recommended Adjustment Practical Starting Range Why It Works Key Check
1. Reduce Axial Depth of Cut Excessive tool engagement increases cutting forces and excites the tool–workpiece system. Reduce axial depth gradually while keeping the radial engagement controlled. Start with 25–50% of the tool diameter for roughing; reduce further if vibration continues. A shorter cutting engagement reduces the total cutting force and can move the operation into a more stable cutting condition. Maintain sufficient material removal for chip formation; avoid rubbing with an extremely light cut.
2. Reduce Radial Engagement Large width of cut produces high instantaneous chip load and unstable cutting forces. Use a lighter radial step-over, especially with long-reach tools or thin walls. Begin around 10–30% of tool diameter for adaptive or high-speed roughing. Lower radial engagement reduces force fluctuations and allows higher spindle speeds in many applications. Verify that the programmed feed is adjusted so the cutter still produces a real chip instead of rubbing.
3. Adjust Spindle Speed The selected spindle speed may coincide with a natural vibration frequency of the tool, holder, or machine. Change spindle speed in controlled increments rather than making only a small random adjustment. Test approximately ±10–20% from the current RPM while monitoring sound, finish, and tool load. Changing tooth-passing frequency can move the process away from a resonant condition. Keep surface speed within the cutting-tool and workpiece material limits.
4. Optimize Feed per Tooth Feed is too high for the available rigidity, or too low and causing rubbing and unstable cutting. Adjust feed per tooth together with spindle speed and radial engagement. Use the tool maker’s recommended chip-load range; change it in 10–15% increments during testing. Correct chip thickness balances cutting force, heat generation, and edge engagement. Calculate feed using: Feed rate = RPM × Number of flutes × Feed per tooth.
5. Shorten Tool Stickout Long tool projection increases deflection and lowers bending stiffness. Use the shortest tool that reaches the feature and reduce unnecessary holder or extension length. Keep stickout as close as practical to the required cutting depth; doubling stickout can greatly increase deflection. Tool stiffness decreases rapidly as unsupported length increases, so a shorter setup strongly improves stability. Check holder cleanliness, taper contact, pull-stud condition, and tool runout before machining.
6. Improve Workholding and Machine Rigidity Part movement, fixture flex, loose fasteners, or poor support allows vibration to develop. Increase clamping support, place clamps close to the cutting zone, and support thin or flexible sections. Keep unsupported wall length as short as possible and use multiple support points where accessible. A rigid workholding system limits relative movement between the cutter and workpiece. Inspect vise or fixture seating, jaw contact, fastener torque, table condition, and workpiece overhang.
7. Use a More Stable Cutting Strategy Sharp entry and exit angles, full-width cuts, or unfavorable tool engagement create sudden force changes. Use climb milling where the machine and setup permit, apply smooth toolpaths, and avoid abrupt direction changes. Prefer constant tool engagement; maintain approximately 10–30% radial engagement for stable roughing trials. Consistent engagement reduces impact loading and produces more uniform cutting forces. Use an appropriate number of flutes and tool geometry for the material; confirm chip evacuation is adequate.

Select and Maintain the Right Milling Tool

Chatter marks often begin with a mismatch between the cutter and cutting conditions. A rigid, suitable tool matters more than simply choosing a larger diameter. For aluminum, polished flutes and adequate chip space can prevent packed chips. Tough alloys may need a stronger edge and fewer flutes. The correct choice depends on material, radial engagement, depth, and machine rigidity. Measure these factors before changing feeds blindly. Small details matter.

Inspect the cutter under bright light before every critical job. A chipped corner, built-up edge, or uneven wear can disturb the cut and leave repeating waves. Check tool runout with a dial indicator; even a small reading can make one tooth cut deeper. Clean the holder and spindle taper carefully. Dirt is not harmless. Use a balanced holder at high spindle speeds, and keep tool projection as short as the setup allows.

Maintenance also requires honest records. Note tool life, material, speed, feed, and the location of chatter marks. When a tool begins to squeal, do not automatically reduce feed. A worn tool may need replacement, while a fresh cutter may need lighter radial engagement or a changed tooth-passing frequency. I have sometimes blamed the machine too quickly. Rechecking clamping and runout often revealed the real cause. After cleaning, inspect the cutting edges again, because a tool can look acceptable and still cut poorly.

Apply Coolant and Improve Chip Evacuation

Coolant management is a practical way to reduce chatter marks during metal milling. Aim the coolant directly at the cutting zone, not merely across the machine table. A steady stream can lower cutting heat and prevent chips from welding onto the tool. Check the concentration regularly, because weak coolant may reduce lubrication and corrosion protection. Too much pressure can also disturb thin parts or push chips into pockets.

Chip evacuation matters just as much. Recutting chips create sudden cutting forces, which often appear as repeating marks on the milled surface. Use enough coolant flow to carry chips away from the tool. In deep cavities, combine coolant with directed air to clear trapped material. A clean flute path helps. Keep the nozzle close, but avoid blocking the operator’s view. Small changes can make a visible difference.

In practice, I would inspect the chips after every trial cut. Long, hot chips suggest poor evacuation or unsuitable cutting conditions. Shorter chips usually indicate better control, though this is not a complete diagnosis. I once increased coolant pressure and saw worse vibration because the stream pushed chips against a pocket wall. That result was a useful reminder: more coolant is not always better. Adjust flow, nozzle position, and cutting parameters together, then compare the surface under consistent lighting.

7 Best Ways to Fix Chatter Marks in Metal Milling: Apply Coolant and Improve Chip Evacuation

This normalized comparison shows how common process improvements can reduce chatter severity in metal milling. Using coolant helps control cutting temperature and friction, while better chip evacuation prevents recutting and chip packing. The lowest chatter index is achieved when coolant delivery and chip evacuation are improved together.

Inspect the Surface and Prevent Future Chatter Marks

Chatter marks should be inspected before any parameter is changed. Under angled light, the surface often reveals repeating waves, torn edges, or bright ridges. I use a clean fingernail check, then compare the mark spacing with the cutter’s tooth pattern. A portable profilometer can record Ra and Rz values, while a microscope exposes chipped edges and built-up material. ISO 21920-2:2021 recommends separating roughness from waviness, which prevents a serious mistake: treating vibration as ordinary surface roughness. The CIRP Journal of Manufacturing Science and Technology has reported that unstable cutting can reduce tool life by up to 50%.

Small details matter. Measure tool runout at the cutting edge, not only at the holder. Check fixture contact, workpiece overhang, and spindle bearings. A loose fixture can leave marks that look like a dull cutter. I have made that mistake before. The machine was not the real problem.

To prevent recurrence, shorten tool stickout and increase workholding stiffness. Test a modest spindle-speed shift, often 10–20%, while keeping feed per tooth controlled. Avoid changing speed and feed together; otherwise, the cause stays unclear. Record the successful settings beside the material, tool diameter, radial engagement, and coolant condition. A 2023 manufacturing-maintenance survey from the U.S. Department of Energy emphasizes that consistent process records support repeatable improvements. Inspect the next part immediately. Chatter can return quietly.

FAQS

: What commonly causes chatter marks during milling?

: Small movements in the workpiece, tool, or machine can create repeating surface waves. The movement may feel invisible. Flexible parts often cause more trouble than expected.

How can I stabilize the workpiece?

Use firm, even clamping across the workpiece. Support thin walls with a suitable fixture or temporary backing. Check for chips beneath the fixture. One small chip can create visible waves.

Why does tool overhang matter?

Keep the tool overhang as short as practical. Long stickout behaves like a spring and increases vibration. Shorter tools usually provide better support. This simple detail is easy to overlook.

What should I inspect before changing cutting parameters?

Check holder seating, tool runout, insert security, and spindle taper condition. Also inspect fixture contact surfaces. A sharp, balanced tool usually improves the finished surface. I have sometimes blamed cutting data too quickly.

How can machine setup affect chatter?

Lock unused axes and verify table and vise rigidity. Avoid cutting near the edge of the machine’s working range. Changing support can change the surface on each side. Measure the finished wall instead of trusting appearance alone.

Should I change spindle speed when chatter remains?

Adjust spindle speed in small steps after checking mechanical stability. Then review feed per tooth and radial engagement. Large changes can hide the real cause. Change one factor carefully.

Where should coolant be directed?

Aim a steady stream directly at the cutting zone. Do not spray only across the machine table. Proper flow can reduce heat and prevent chips from welding onto the tool. More pressure is not always better.

How does chip evacuation influence surface quality?

Recutting chips create sudden cutting forces and repeating marks. Use enough coolant to carry chips away from the tool. For deep cavities, directed air can clear trapped material. Keep the nozzle close, but protect the operator’s view.

What do the chips reveal after a trial cut?

Long, hot chips may indicate poor evacuation or unsuitable cutting conditions. Shorter chips often suggest better control. They do not provide a complete diagnosis. Inspect the surface under consistent lighting and compare results carefully.

Conclusion

Chatter marks in metal milling are usually caused by vibration from an unstable workpiece, weak machine setup, incorrect cutting conditions, worn tooling, or poor chip removal. To understand how to fix chatter marks in metal milling, begin by checking that the workpiece, fixture, tool holder, and machine are firmly secured. Then adjust spindle speed, feed rate, and cutting depth gradually to reduce vibration and maintain a smoother cutting action. Selecting the correct tool geometry and keeping the tool sharp can also improve stability and surface quality.

Effective coolant application and proper chip evacuation help prevent recutting, heat buildup, and additional vibration. After machining, inspect the surface for repeating lines, irregular patterns, or localized damage to identify the source of the chatter. Record the successful cutting settings, maintain the machine and tooling regularly, and review the setup before future operations. A stable system, suitable cutting parameters, and consistent maintenance are the key to producing cleaner, more accurate milled surfaces.
Charlotte

Charlotte

Charlotte is a seasoned marketing professional with a deep understanding of the company's portfolio and a passion for elevating its presence in the market. With a keen eye for detail and a commitment to excellence, she ensures that our professional blog is regularly updated with insightful articles......